 English
Smart Supply Chain Solutions for Hot Chocolate Mix Suppliers

Introduction
The supply chain for any product involves more than a recipe. Hot chocolate has to maintain the same taste, arrive in the same condition, and use the same materials as in any other batch. This factor is relevant to any Hot Chocolate Mix Suppliers, who base their production on cocoa, sugar, milk powders, flavouring agents, and other materials. Additionally, the packaging, storage, and delivery of a product also require special consideration.
A properly structured supply chain addresses the relations between purchase, production, warehouse, quality control, packing, and distribution functions. Instead of responding to urgencies in production or delivery, a company can address them in advance, based on demand forecasts and current stock levels.
Understanding Demand Before Purchasing
Demand forecasting represents one of the key practices, allowing supply chain management to become safe and efficient. The demand for hot chocolate mix depends on the season, weather, marketing, holidays, and retail trends. It may vary significantly for a supplier of café products compared to a company selling chocolate mix online or in retail stores.
Historical sales data helps in identifying demand patterns and establishes the basis for purchase planning. For instance, increased demand during cold seasons and months allows for advancing cocoa and packaging material purchases. In its turn, the forecast becomes even more accurate with the input of current orders, distributor estimates, and marketing activities.
It is worth noting that demand forecasting does not equal overstocking: purchasing raw materials and components is planned in a way that leaves an option for demand changes. Thus, the hot chocolate mix production receives the necessary number of materials, avoiding extra inventory.
Smarter Raw Material Procurement
The purchase of raw materials and components is another essential element of supply chain management. Cocoa powder, sugar, dairy products, and flavours: these and many other ingredients must have reliable suppliers, who can provide the necessary quality of goods and document it. It is also important to plan purchases considering the time-horizon, volumes, storage conditions, and costs of materials, not only the current price.
For ingredients with a large procurement cycle, the option of safety stock is suitable as a safeguard against out-of-stock situations. At the same time, the size and dynamics of safety stock must be related to actual consumption and supplier performance to avoid inventory buildup.
Inventory Visibility Across Operations
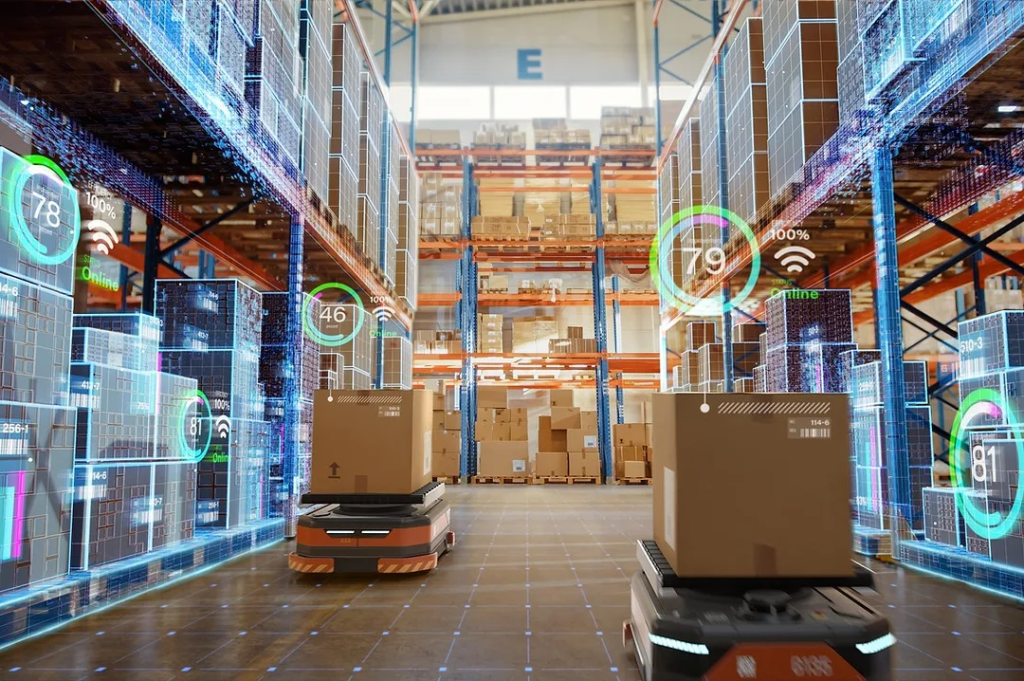
Inventory management ensures the smooth operation of the supply chain by maintaining the balance between demand and material availability. A well-organized system, possibly supported by digitization, helps track the current level of materials, work-in-progress, and finished goods.
Batch tracking is another useful practice, especially for food production, where it is needed to follow the flow of ingredients. For example, the hot chocolate mix components, processed in certain batches, receive dates, and end up in products of a particular size and quantity. It allows recalling items in case of quality issues or managing batch rotation in a way, that first-expired materials are used first.
In addition, inventory management supports warehouses, where finished goods are stored, packed, or subjected to further quality control. First-expiry-first-out rules help minimize losses with high-value materials and goods, while regular inventory counts support the reconciliation of counts with actual stock.
Efficient Production Scheduling
Production planning and scheduling are essential for the hot chocolate mix supply chain because they prevent over- or under-production of materials. Both have negative effects: the former ties up inventories, while the latter complicates the fulfillment of customer orders. The current level of finished goods and work-in-progress, as well as the planned sales volume, helps set priorities in production planning.
At the same time, the production schedule should consider practical conditions, such as the capabilities of machinery, sizes of production batches, cleaning and maintenance, labor force, materials availability, and delivery planning. Combining similar batches of production allows avoiding idle time between them due to equipment changeover. Moreover, the time to conduct quality control, document, pack, and label products also needs to be accounted for: it determines the earliest possible date of delivery.
Warehouse Design and Storage Control
Warehouses accommodate materials and goods in storage, which is why their organization and safety conditions are essential. Storages should have designated areas for materials and goods, with controlled temperature, humidity, and other environmental conditions. Cocoa powder, for example, is susceptible to dampness, leading to clumping and lower quality; incorrect storage conditions may also cause the need for quality control and customer complaints.
Hot chocolate mix production: raw materials, work-in-progress, and finished goods require appropriate packaging, which also documents certain properties of the items. Therefore, warehouses benefit from climate control and regular inventory to keep track of materials and prevent the expiration of goods. Finally, the design of warehouses and storage enables faster operations, reducing the time between the receipt of an order and its fulfillment.
Reliable Packaging and Dispatch
The packaging of finished products is part of the production process in hot chocolate mix manufacturing establishments. However, its disruption, for example, due to paper stockout, may halt the entire production line, even if there are available materials and components. Thus, the inventory of packaging materials should be aligned with consumption to prevent idle time of the production line. It is also vital to control the quality of packaging materials and label content to avoid errors in size, quantity, or product name.
In its turn, dispatch ensures that the correct quantity and quality of goods are delivered to the customer within the deadline. Barcode scanning assists in fulfilling this obligation by reducing human error when packing, shipping, and receiving goods. For multiple sizes and formulations, barcode scanning becomes a helpful tool to ensure that all items are delivered to the correct address.
Using Data to Improve Decisions
Data collected within the supply chain helps in identifying patterns and making decisions to optimize operations. There are many sources of data, including purchase planning, inventory control, production scheduling, and sales, which all connect and affect each other. This interrelation is why the analysis of collected data becomes a helpful tool for supply chain management.
The main indicators for the analysis cover inventory turnover, demand forecast accuracy, fulfillment rate, supplier lead time, production yield, and stock-out frequency. The interpretation of data depends on the current performance of the supply chain, where some of the indicators may signalize potential issues.
For example, if there is a frequent occurrence of stockouts, it indicates problems with the demand forecast and purchase planning, which requires readjusting to prevent disruptions. At the same time, inventory buildup speaks of over-purchasing and inaccurate forecast, which is unsafe for the supply chain.
Building Supplier Resilience
Supply chain disruptions may occur due to various reasons, such as transportation issues, seasonal product shortages, price fluctuations, technical failures, or demand surges. It is necessary to anticipate random events and ensure that the supply chain can sustain itself in any situation.
An example of such a measure applies to the Hot Chocolate Mix Suppliers and the choice of suppliers for cocoa powder, sugar, dairy products, and other ingredients and packaging components. Although it may seem that a single supplier can be relied upon with a long-term contract, diversifying supply sources prevents disruptions.
Technology Without Unnecessary Complexity
Software and technology in supply chain management is not compulsory, despite its benefits for operational efficiency and organization. However, a functional inventory and production platform can assist in many tasks with sufficient data input. It is vital to choose the software, which offers a variety of tools, including purchase planning, batch tracking, inventory management, and barcode recognition.
The integration of these tools eliminates the need for separate platforms and reduces errors due to manual data entry. In addition, a software solution assists in analyzing inventory turnover, production yield, fulfillment rate, and other indicators, which contribute to the optimization of supply chain performance.
For growing Hot Chocolate Mix Suppliers, supplied from an integrated software, grows in scale alongside the company’s needs without the need for complex and costly solutions. The primary advantage of technology is the availability of information, which becomes helpful for decision-making.
Quality and Supply Chain Working Together
Quality management supports the smooth operation of the supply chain by reducing quality defects, which disrupt production, inventory control, and customer relations. As a result, quality planning needs to include suppliers of raw materials and components, production processes, and documentation of finished goods.
Documentation, in particular, helps operate supply chain management and quality control within the hot chocolate mix production. Batch records, supplier documents, test results, and dispatch data provide a full history of each product batch and assist in addressing any customer concerns.
Choconutri specializes in chocolate products and offers various solutions for desserts and drinks. It covers the needs of customers in the food industry, who value the quality of ingredients and the convenience of production.
Conclusion
Supply chain management is the backbone of hot chocolate mix suppliers, offering control over costs, inventory, production, quality, and delivery. Demand forecasting assists in purchase planning, while batch tracking and inventory management provide control over materials and prevent disruptions. An efficient production schedule reduces the time spent on manufacturing, and organized warehouses sustain product quality with minimal inventory buildup.
The best supply chains are those, which operate smoothly and reliably, preventing risks and issues. In this regard, data, suppliers, processes, and technology all combine and support each other in creating a strong supply chain management system. The analysis of demand and inventory, production scheduling, and delivery performance become helpful insights on the way to building sustainable operations in hot chocolate mix manufacturing.